How to Choose Cast Steel Valves for Global Projects?

Choosing cast steel valves for global projects demands more than comparing price, pressure class, and delivery time. Each valve must survive the actual service: abrasive slurry, hot steam, sour gas, seawater, or repeated cycling. Grand View Research and MarketsandMarkets both report continued growth in the global industrial valves market, although their estimates differ because market definitions vary. That difference deserves attention. It reminds engineers that supplier claims should never replace project-specific verification.

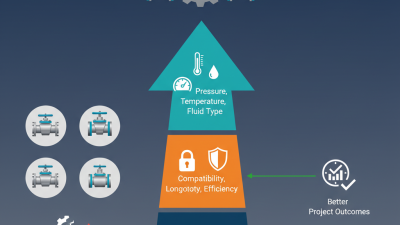
Peter Smith, co-author of Valve Selection Handbook, offers a practical principle: “Select the valve for the service, not merely for the line size.” The advice remains relevant when selecting cast steel valves for refineries, power stations, pipelines, and water infrastructure. A 24-inch valve may fit the drawing, yet fail early if its trim ignores chloride exposure or erosive particles. The datasheet must show pressure-temperature ratings, body material, trim grade, seat design, end connection, testing, and coating requirements.

Global compliance adds another layer. API 600, ASME B16.34, ISO 15848-1, and NACE MR0175/ISO 15156 may apply, depending on service and location. Certification should be traceable to heat numbers, inspection records, and pressure-test results. Independent reports can indicate market direction, but they cannot confirm one manufacturer’s quality. That is the uncomfortable part. Selection is never perfectly risk-free. However, disciplined specifications, witnessed testing, and realistic maintenance planning make the risk visible and manageable. A robust decision begins with operating conditions, not a catalogue photograph.

How to Choose Cast Steel Valves for Global Projects?

Project Requirements and Valve Service Conditions

How to Choose Cast Steel Valves for Global Projects?

Project requirements must guide every cast steel valve decision. Start with the medium, pressure, temperature, flow direction, and operating frequency. Steam at 420°C needs different trim than seawater at ambient temperature. Sour gas also requires material evaluation under NACE MR0175/ISO 15156. Do not select by pressure class alone. Check wall thickness, corrosion allowance, end connections, and actuator torque. In practice, a valve can pass factory tests yet fail during startup because the project ignored low-temperature impact requirements. That mistake is expensive.

Global projects also need traceable quality records. Specify positive material identification, heat numbers, radiography levels, hydrostatic testing, and fugitive-emission testing. The IEA’s Global Methane Tracker 2024 estimates that around 40% of fossil-fuel methane emissions could be avoided without a net cost. This makes stem sealing and packing selection more important, especially on gas facilities. API 6D, ASME B16.34, and ISO 15848 can support consistent technical requirements across suppliers. However, standards do not replace site-specific judgment.

Tips: Build a service-condition table before requesting quotations. Include minimum and maximum pressure, temperature, fluid chemistry, solids content, cycling frequency, and installation altitude. Ask for test procedures, not only certificates. Review maintenance access around the handwheel and drain points. One detail is often missed: verify valve orientation after insulation. A perfect specification can still become impractical in the field.

Cast Steel Grades and Material Selection Criteria

For global projects, cast steel selection begins with pressure, temperature, and fluid chemistry. ASTM A216 WCB suits many carbon-steel valves for moderate and high-temperature service. WCC offers higher tensile strength, but it is not automatically the better choice. Low-temperature systems often require ASTM A352 LCB or LCC, with impact testing at specified temperatures. For elevated heat, ASTM A217 WC6 or WC9 may provide stronger creep resistance.

Corrosion deserves equal attention. The NACE IMPACT Study estimated global corrosion costs at approximately US$2.5 trillion annually, or 3.4% of global GDP. That figure makes material review more than a purchasing exercise. For sour service, engineers should evaluate hardness, heat treatment, and qualification against ISO 15156/NACE MR0175. Chlorides may demand stainless or duplex cast grades, such as ASTM A351 CF8M or ASTM A995 grades. However, “stainless” does not mean corrosion-proof.

A practical specification should define design pressure, minimum design temperature, chloride level, hydrogen sulfide exposure, weld-repair limits, and inspection requirements. I have seen grade tables hide important gaps. A stronger grade may still fail after poor casting quality or unsuitable trim selection. Project teams should verify MTRs, impact results, radiography, and pressure-test records. ASTM, ASME, and project specifications must align. One overlooked temperature value can change the entire valve material decision.

How to Choose Cast Steel Valves for Global Projects?

Cast steel grade selection should consider pressure class, design temperature, corrosion exposure, weldability, impact requirements, and applicable standards. The chart compares minimum mechanical properties commonly specified for ASTM A216 and ASTM A217 cast steel grades.

WCB and WCC are carbon steel grades commonly selected for general hydrocarbon and utility service. WC6 and WC9 are chromium-molybdenum alloy steels intended for elevated-temperature service. C5 is a higher-chromium alloy grade used where improved oxidation and corrosion resistance is required. Values shown are minimum specified tensile and yield strengths at room temperature; project standards and temperature derating requirements must be checked before final selection.

Pressure Classes, Standards, and Certification Requirements

How to Choose Cast Steel Valves for Global Projects?

Pressure Classes, Standards, and Certification Requirements

Choosing a cast steel valve starts with the pressure-temperature envelope, not the catalog size. Define design pressure, operating temperature, fluid, corrosion allowance, and shutoff duty. ASME Class 150, 300, 600, and higher ratings are not interchangeable with PN values. Their allowable pressures change with temperature and material grade. Use the project design code and verified rating tables. Do not convert Class 300 to PN16 by habit. That shortcut can create a serious design error.

Standards must match the service and destination. Common references include ASME B16.34 for valve design, API 600 for certain bolted-bonnet gate valves, and ISO 5208 for pressure testing. European projects may require EN specifications and conformity assessment under applicable regulations. Confirm whether the contract demands fire testing, fugitive-emission testing, sour-service controls, or low-temperature impact tests. The datasheet should state every requirement clearly.

Certification is more than a stamped certificate. Request material test reports, heat-number traceability, dimensional records, calibration evidence, and hydrostatic test results. Independent inspection may witness casting quality checks, radiography, ultrasonic testing, and final testing. Check the certificate scope, issuing body, revision, and product identity. A document copied from another heat is useless. Match body markings, tag numbers, drawings, and test records before shipment. Small discrepancies deserve review, not optimism. Even experienced teams can miss a conflicting standard edition.

Valve Design Features for Safety and Operational Reliability

Choosing cast steel valves for global projects requires more than pressure and size matching. Design details often decide whether a valve survives years of cycling, vibration, and temperature changes. I specify body materials against process chemistry, design pressure, and minimum temperature. Wall thickness should follow recognized requirements, such as API 600 and ASME B16.34. Radiographic examination also helps reveal hidden casting defects. Small defects can become expensive failures.

Stem sealing deserves close attention. ISO 15848-1 testing supports the evaluation of fugitive emissions during temperature and pressure cycling. The IEA Global Methane Tracker 2024 reported that about 40% of fossil-fuel methane emissions could be reduced at no net cost. That makes low-emission packing, live-loaded glands, and accurate stem finishes practical safety features, not decorative upgrades. Double isolation and bleed arrangements can improve maintenance safety, but only when operators can verify their position clearly.

Corrosion control needs equal discipline. The NACE IMPACT study estimated global corrosion costs at about 2.5 trillion dollars annually, or 3.4% of global economic output. Select trim alloys carefully, especially for sour, chloride-rich, or wet service. Drainable cavities reduce trapped fluids and freezing risks. Fire-safe design, anti-static continuity, and fail-position logic support safer shutdowns. Yet no design is perfect. Field access may remain poor, and inspection assumptions may be optimistic. A commissioning review should challenge both.

Supplier Evaluation, Testing, and Global Delivery Planning

Choosing cast steel valves for a global project starts with evidence, not attractive quotations. An experienced supplier should show relevant project records, qualified personnel, and controlled manufacturing procedures. Request heat-number traceability from steel casting to final assembly. Review material certificates, welding qualifications, and dimensional inspection reports. Confirm pressure ratings, temperature limits, trim materials, and end connections against the project specification.

Testing must be planned before production begins. The inspection and test plan should define hydrostatic testing, shell testing, seat leakage limits, and non-destructive examination. Witness points should be clear for the purchaser, inspector, and supplier. Ask for calibrated equipment records and complete test reports. Do not accept vague compliance statements. Small gaps matter.

Global delivery requires more than a factory dispatch date. Check production capacity, raw material availability, export documentation, and port routing. Use protective end caps, sealed packing, and corrosion-resistant packaging for long sea voyages. Include valve tags, spare parts, installation instructions, and digital records in the shipment. A realistic schedule should contain buffer time for inspection and customs clearance. Even a strong plan can miss a vessel connection. That risk deserves attention. Supplier evaluation is not a one-time questionnaire; it is a practical review of communication, technical judgment, and response speed when details change.

How to Choose Cast Steel Valves for Global Projects? - Supplier Evaluation, Testing, and Global Delivery Planning

Category Evaluation Dimension Recommended Requirement or Benchmark Verification Evidence Planning Data
1. Supplier Evaluation
Technical Capability Product range and pressure capability Ability to manufacture cast steel gate, globe, and check valves for ASME Class 150, 300, 600, and 900 applications, subject to project design conditions. Approved valve data sheets, dimensional drawings, pressure-temperature ratings, and previous project references with identifying information removed. Target technical compliance: 100% of approved valve specifications
Material Control Body and trim material traceability Use project-approved materials such as ASTM A216 WCB for carbon steel bodies and ASTM A351 CF8M for corrosion-resistant cast bodies, where specified. Heat numbers, material test certificates, casting records, chemical analysis, mechanical test results, and positive material identification reports. Traceability coverage: 100% from casting heat to finished valve
Quality System Quality management and inspection readiness Documented quality procedures, calibrated inspection equipment, nonconformance control, corrective-action procedures, and customer inspection support. Current quality certificate, quality manual, internal audit records, calibration certificates, and sample inspection and test plans. Calibration validity: 100% at the time of inspection
Manufacturing Capacity Capacity for project volume and peak demand Demonstrated casting, machining, assembly, coating, testing, and packing capacity for the required valve sizes and quantities. Capacity statement, production schedule, machine list, subcontractor register, and bottleneck analysis. Recommended capacity reserve: at least 15% above the confirmed project requirement
Documentation Manufacturing record book quality Documentation should cover approved drawings, inspection plans, material certificates, welding records, NDE reports, pressure test records, coating reports, and final release certificates. Document register, sample manufacturing record book, revision-control procedure, and document-transmittal log. Document submission target: within 5 working days after each inspection milestone
2. Testing and Inspection
Pressure Testing Shell, body, and seat testing Perform hydrostatic shell and seat tests in accordance with the approved project standard, commonly API 598 or an equivalent specified standard. Approved test procedure, calibrated pressure gauges, test charts, test-duration records, leakage results, and signed inspection reports. Acceptance target: no visible external leakage; seat leakage within the applicable standard limit
Nondestructive Examination Casting and weld integrity Apply radiographic, ultrasonic, magnetic-particle, or liquid-penetrant examination according to the approved inspection plan and casting class. NDE procedures, operator qualifications, equipment calibration, examination reports, and repair records where applicable. Minimum coverage: as defined by the project ITP; critical pressure-retaining areas require documented examination
Positive Material Identification Verification of alloy and trim materials Conduct PMI on pressure-retaining and specified trim components when required by the material specification or project risk assessment. PMI reports linked to part numbers, heat numbers, and valve serial numbers. Traceability target: 100% of PMI-designated components
Functional Testing Operation and dimensional conformity Verify opening and closing operation, stem travel, handwheel or actuator orientation, face-to-face dimensions, flange drilling, and flow-direction markings. Final inspection checklist, dimensional report, operating-torque record where required, and photographic evidence. Functional acceptance: 100% of finished valves before release
Special Service Testing Fire-safe, fugitive-emission, cryogenic, or sour-service requirements Add special tests only when required by the service conditions, applicable standards, or project specifications. Type-test certificates, fire-safe test reports, fugitive-emission test reports, low-temperature impact results, or sour-service material compliance records. Testing scope: risk-based and defined before purchase-order release
3. Global Delivery Planning
Lead-Time Planning Manufacturing and inspection schedule Build the schedule from drawing approval, raw-material procurement, casting, machining, assembly, testing, documentation, and packing. Level-3 production schedule, milestone tracker, expediting reports, and recovery plan for delays. Typical planning range: 12–24 weeks after approved technical documents, depending on size, material, quantity, and testing scope
Inspection Coordination Hold points and witness points Schedule customer, third-party, or remote inspections with adequate notice and clearly defined release conditions. Approved inspection and test plan, inspection notification forms, release notes, and punch-list closure records. Recommended notice: 5–10 working days before planned inspection activities
Export Packaging Protection during multimodal transport Use corrosion protection, flange-face covers, sealed openings, moisture-resistant packing, lifting points, and export-grade crates or pallets. Packing specification, packing-list photographs, crate markings, gross and net weights, and lifting instructions. Packaging objective: protection for sea, road, rail, or air transport under the agreed shipping route
Shipping Documents Customs and destination-country requirements Prepare commercial invoice, packing list, transport document, certificate of origin where required, insurance documents, export classification, and technical dossier. Pre-shipment document checklist reviewed by logistics and the receiving party. Document accuracy target: 100%; submit draft shipping documents at least 3 working days before dispatch
Logistics Risk Route, port, customs, and disruption exposure Assess transit time, port congestion, sanctions or trade restrictions, seasonal weather, customs requirements, and availability of alternative routes. Logistics risk register, route comparison, contingency plan, and shipment tracking procedure. Recommended schedule contingency: 10–20% of planned transit and handling time
After-Sales Support Warranty, spare parts, and technical response Define warranty terms, replacement-part availability, technical query response time, failure investigation, and corrective-action responsibilities. Warranty statement, spare-parts list, service procedure, escalation contacts, and nonconformance response template. Technical query response target: within 2 working days; corrective-action proposal: within 10 working days
4. Recommended Supplier Scoring Model
Weighted Score Technical compliance Evaluate material suitability, design compliance, pressure class, applicable standards, and special-service capability. Technical bid evaluation and deviation list. Suggested weight: 30%
Weighted Score Quality and testing performance Evaluate inspection capability, test coverage, traceability, documentation quality, and historical nonconformance performance. Quality assessment, sample manufacturing record book, and inspection audit. Suggested weight: 25%
Weighted Score Delivery reliability Evaluate realistic lead time, capacity reserve, expediting discipline, logistics planning, and contingency arrangements. Production schedule, capacity review, and delivery-performance records. Suggested weight: 20%
Weighted Score Commercial competitiveness Compare total delivered cost, payment terms, tooling or testing charges, packaging costs, warranty terms, and change-order exposure. Commercial bid comparison and total-cost-of-ownership worksheet. Suggested weight: 15%
Weighted Score Communication and support Evaluate response speed, engineering support, document control, language capability, and escalation effectiveness. Tender clarification log, communication test, and project-support plan. Suggested weight: 10%
Total Recommended Evaluation Weight 100%
×
img

    Contact Info

    Phone number

    661-392-8948

    Address info

    3451 Pegasus Drive, Bakersfield, CA USA