Blog
- Home
- Blog
7 Best Wellhead Valves for Oil and Gas Buyers
Wellhead valves sit at the pressure boundary between a producing well and surface equipment. They control flow, support isolation, and help crews manage demanding operating conditions. At a remote pad, a leaking connection or difficult-to-turn handwheel can mean lost production and extra service work. The consequences are tangible.
The International Energy Agency’s Oil 2024 report projects oil demand growth of 3.2 million barrels per day by 2030, nearing 106 million barrels per day. Its World Energy Investment 2024 report estimates global upstream oil and gas investment at about $570 billion in 2024, a 7% increase. These figures do not predict demand for any particular valve. They do show why equipment selection remains a practical concern for operators and buyers.
This guide reviews seven wellhead valve options through the details that matter in the field: pressure rating, temperature range, materials, end connections, actuation, and serviceability. It also points buyers toward relevant requirements, including API Spec 6A and ISO 10423, while recognizing that project specifications and operating environments differ. For sour-service applications, ISO 15156 may also be relevant; confirm its applicability with qualified engineering personnel. A catalog rating alone is not enough. Check the actual configuration, documentation, and maintenance needs before comparing suppliers. Some differences look minor on a datasheet. They may not feel minor during installation. The right choice depends on the well, the operating plan, and the evidence behind the product claims.
Wellhead Valve Fundamentals: API 6A Pressure Classes from 2,000 to 20,000 psi
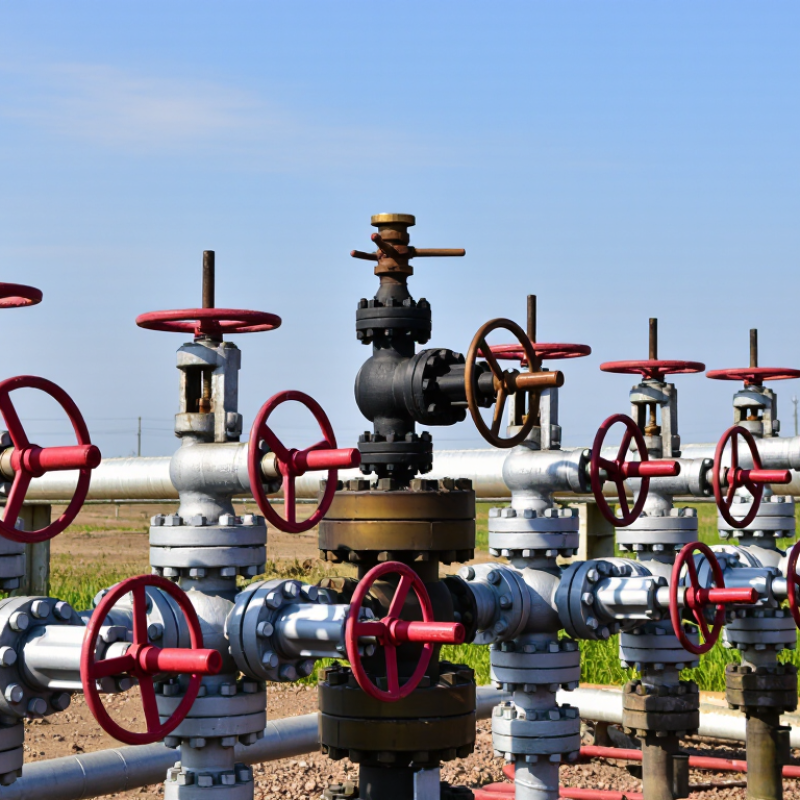
API Spec 6A, 21st edition, lists rated working-pressure classes of 2,000, 3,000, 5,000, 10,000, 15,000, and 20,000 psi. These are equipment ratings, not targets for routine operation. A 10,000-psi valve, for example, must suit the well’s expected pressure and service conditions; choosing by pressure alone is not enough. Small distinction. Big consequence.
Buyers should check the full wellhead specification: pressure rating, temperature range, material class, connection type, and fluid compatibility. Sour service and abrasive production fluids can change material and trim requirements. Confirm the valve’s rated working pressure against the well design, including credible pressure scenarios, rather than relying only on typical readings. API 6A provides the rating framework, but project-specific engineering determines the right selection.
Before purchase, review the manufacturer’s documentation for traceability, inspection, and pressure-test records against the applicable API 6A requirements. Ask how seals and operating components are qualified for the stated service. Field conditions rarely match a neat spreadsheet. That judgment deserves a second look. A higher pressure class may add cost and impose different equipment requirements, while an underspecified valve creates an avoidable integrity risk. Source: API Specification 6A, Specification for Wellhead and Tree Equipment, 21st edition.
Seven Valve Types Compared: Gate, Choke, Ball, Check, Plug, Safety, and Needle
Wellhead valves serve different duties, and similar-looking bodies can behave very differently under pressure. The U.S. Energy Information Administration reported record crude oil production of about 13.2 million barrels per day in 2024. That scale makes dependable isolation and pressure control more than a catalog detail. (EIA, Short-Term Energy Outlook, January 2025.)
Small detail, real consequence.
API Specification 6A and ISO 10423 provide requirements for wellhead and tree equipment; buyers should match pressure class, temperature, materials, and sour-service needs to documented operating conditions. Do not treat a standard as proof that every valve suits every well. A practical review includes pressure ratings, sealing materials, actuator needs, inspection access, and maintenance history. Even a technically compliant choice can be wrong for a particular well. The operating data may be incomplete, and that uncertainty deserves a second look.
Match Valve Design to Well Service, Flow Control, and Shutoff Requirements
Choosing a wellhead valve begins with the service, not the catalogue ranking. Production, injection, testing, and shut-in duties place different demands on flow control and isolation. A gate valve is commonly selected for firm on-off service, while a choke valve helps regulate flow and manage pressure drop. Check valves can limit reverse flow where the system design requires it. Small details matter.
Compare pressure and temperature limits with actual operating and upset conditions. Review fluid composition, solids, corrosion risks, and required shutoff performance. A valve that suits clean service may wear faster when sand or abrasive particles are present. Confirm materials, connection type, actuation, and maintenance access against documented specifications. Not always obvious.
In the field, a stiff handwheel or hard-to-reach actuator can turn routine isolation into a delay. I would also check how often the valve must cycle; a rarely operated shutoff valve has different needs from a frequently adjusted control point. Match each position on the wellhead to its function, then verify selection with qualified engineering review and site records. A spreadsheet can miss this.
7 Best Wellhead Valves for Oil and Gas Buyers - Match Valve Design to Well Service, Flow Control, and Shutoff Requirements
| Valve design | Typical well service | Flow and shutoff characteristics | Why buyers consider it | Selection considerations |
|---|---|---|---|---|
| 1. Wedge gate valve | Wellhead and tree isolation in production or service applications where a gate-style valve is specified. | Designed primarily for fully open or fully closed service. When fully open, the gate retracts from the flow path; it is generally not intended for routine throttling. | A familiar isolation design that can provide a straight-through flow path when open. | Confirm pressure and temperature ratings, end connections, materials, sealing arrangement, and compatibility with the well fluid. Avoid using it as a control valve. |
| 2. Slab gate valve | Production trees and other wellhead or high-pressure applications that call for a through-conduit gate design. | The gate moves across the bore for on/off service. Through-conduit designs can maintain a relatively unobstructed bore when open; they are not normally used for throttling. | The straight-through bore can be useful where minimizing flow-path obstruction or allowing compatible intervention tools through the valve is important. | Check the specific design’s sealing behavior, operating torque, bore dimensions, and suitability for the expected solids, pressure, and cycling frequency. |
| 3. Expanding gate valve | Wellhead isolation duties where the selected valve design uses mechanical expansion of the gate and segment to seat. | An on/off design. The gate assembly expands against the seats in the closed position; performance depends on the particular design and pressure conditions. | Can provide positive seating characteristics in applications matched to the valve’s specified operating envelope. | Verify whether the valve is designed for bidirectional sealing, how pressure affects seating, and what maintenance and operating procedures are required. |
| 4. Through-conduit gate valve | Tree or flowline isolation where a full-bore or otherwise specified continuous passage is needed. | Provides a continuous bore when open in designs intended for that purpose. Intended mainly for isolation, not for regulating flow by partial opening. | A practical choice when bore continuity and access for compatible tools are key requirements. | Confirm the actual bore size and tool compatibility; “through-conduit” does not by itself establish a particular pressure rating or suitability for every intervention. |
| 5. Ball valve | Selected wellhead, flowline, or auxiliary isolation duties where the valve’s pressure, temperature, and service ratings are suitable. | Quarter-turn operation; a bored ball aligns with the flow path when open and rotates across it to close. Generally used for on/off service rather than continuous throttling. | Fast operation and a compact operating motion can suit applications where quarter-turn actuation is useful. | Do not assume every ball valve is suitable for wellhead pressure or abrasive, sour, or high-temperature service. Check seat and body materials, fire-safe requirements where applicable, and end connections. |
| 6. Choke valve | Production flow control on a well tree or choke manifold, including reducing or adjusting flow and managing pressure drop. | Designed to regulate flow through a variable restriction. It is a flow-control device and should not automatically be treated as the sole positive isolation valve. | Purpose-built for controlled throttling, unlike ordinary gate valves that are generally intended for open-or-closed operation. | Select trim and body configuration for expected pressure drop, flow rate, fluid properties, erosion risk, and control method. Use separate isolation where required by the operating procedure. |
| 7. Check valve | Specified locations in wellhead-associated piping or equipment where reverse-flow prevention is required. | Allows flow in the intended direction and closes in response to reverse flow. It operates automatically and is not a substitute for a manually operated isolation valve. | Can help limit backflow without routine operator actuation when correctly sized and installed. | Confirm flow direction, cracking or opening behavior, allowable pressure drop, orientation limits, and suitability for the fluid and operating conditions. |
Selection note: “Best” depends on the well’s pressure and temperature envelope, fluid composition, solids or erosion exposure, required flow control, shutoff duty, actuation, and applicable specifications. Verify the valve’s documentation and ratings for the exact service; designs and capabilities vary by configuration.
Verify API 6A PSL, Material Class, Temperature Class, and Connection Ratings
7 Best Wellhead Valves for Oil and Gas Buyers
When comparing wellhead valves, verify the paperwork against the actual service conditions. API Specification 6A sets requirements for wellhead and tree equipment, including pressure ratings, materials, and quality controls. PSL indicates specified quality-control requirements; it is not a simple guarantee of field life. Request the manufacturer’s documentation and confirm the stated PSL matches the purchase specification. Small mismatches matter.
Check the material class against the produced fluids and expected corrosion exposure. For sour service, do not assume the class alone establishes suitability; confirm applicable material requirements and project specifications. Then compare the temperature class with both operating extremes and likely temperature cycling. A valve may meet pressure requirements yet fall outside the site’s temperature envelope. Easy to overlook.
Connection ratings must match the mating equipment in type, size, and pressure rating. Verify these details on drawings and certificates, not only in a catalog description. The IEA’s World Energy Investment 2024 report projected upstream oil and gas investment at about $570 billion for 2024, underscoring the scale of equipment procurement. That figure does not determine valve selection, but it makes disciplined specification checks worthwhile. I would still recheck every interface before ordering.
7 Best Wellhead Valves for Oil and Gas Buyers — Verify API 6A PSL, Material Class, Temperature Class, and Connection Ratings
API 6A nominal working-pressure classes range from 2,000 to 20,000 psi. Use the chart as a reference when comparing valve options; the required rating depends on the well’s design and service conditions.
Before purchase, verify the valve’s documented PSL, material class, temperature class, and end-connection rating against the project requirements. Pressure class alone does not establish suitability. Ratings shown are API 6A nominal working-pressure classes.
Assess Pressure Testing, Maintenance Needs, and Lifecycle Cost Before Purchase
7 Best Wellhead Valves for Oil and Gas Buyers
A valve’s purchase price is only one part of its cost. Before comparing wellhead gate, check, or choke valves, match the pressure rating and materials to the actual service conditions. API Specification 6A provides requirements for wellhead and tree equipment, including pressure testing. Ask for test records tied to the valve’s serial number, plus clear acceptance criteria. A test certificate without traceable details is not enough.
Tips: Compare pressure-test procedures, not just advertised ratings. Check whether the supplier documents test medium, pressure, hold time, and results. Also ask how seals and trim can be inspected or replaced in the field. McKinsey Global Institute’s 2015 report estimated predictive maintenance could reduce maintenance costs by 10–40% in suitable industrial settings. That is a broad industry estimate, not a guaranteed saving for wellhead valves. Still, it shows why service access and inspection planning deserve a place in the purchase review.
Estimate lifecycle cost across expected operating years. Include installation, routine inspection, spare parts, downtime exposure, and removal or repair costs. Compare those estimates under the same operating assumptions; otherwise, the cheaper option may only look better on paper. The spreadsheet rarely tells the whole story. Review failure history and maintenance records from similar service conditions where available. If key data is missing, say so—and treat the estimate as uncertain rather than precise.
Related Posts
-
Top Digital Valves Components You Need to Know?
-
What is a Single Valve and How Does it Work?
-
What are the Benefits of Using Valve Steel in Manufacturing?
-
How to Choose the Right T Valve for Your Plumbing System?
-
Understanding the Role of Gate Valves in Modern Plumbing Systems
-
What is Steel Valves and How They Benefit Your Industrial Applications
(780) 669-9420